← All projects
Project 02 of 07
June 2025
Cutting force
and tool temperature
Fundamentals of Mechanical Manufacturing
Teacher Hu Teng
Team of four, including Md Mithun
*
Machining
*
Finite element analysis
*
Johnson-Cook
*
Audit
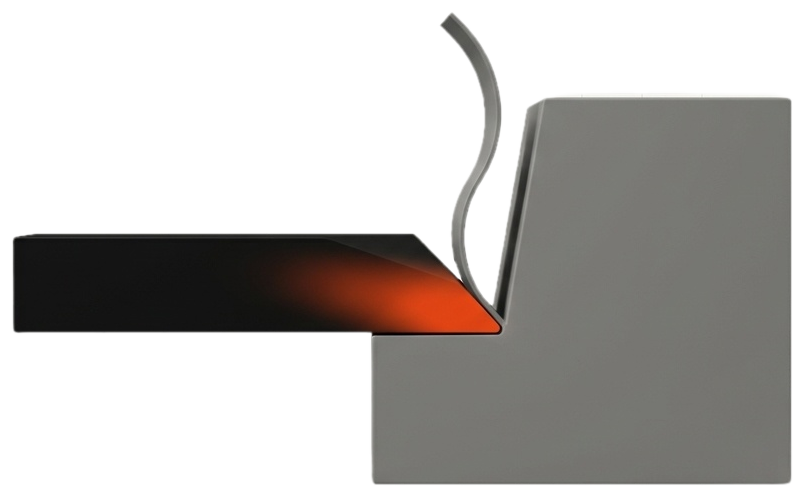
We took a published finite element study of high-speed cutting of AISI 4340 steel, reproduced its logic and audited it. I checked the numbers against Merchant theory and handbook data.
+
01
0 to 20°
of rake angle studied
+
02
300, 433, 550
cutting speeds in m/min
+
03
20 to 28%
lower cutting force as the rake angle rises
What
I did
01
Read the ABAQUS/Explicit Johnson-Cook study line by line.
02
Compared its trends with Merchant theory.
03
Checked its input values against handbook data.
04
Redrew its force and temperature plots so they can be compared at a glance.
+ Honest result
Where it fell short
I found input values that disagree with handbook data, and statements that do not match the plotted curves. I report both in the audit. The plots on this page are my redrawing of values I read off the source study's figures, so they carry a reading uncertainty of about 30 N and 10 degrees Celsius.
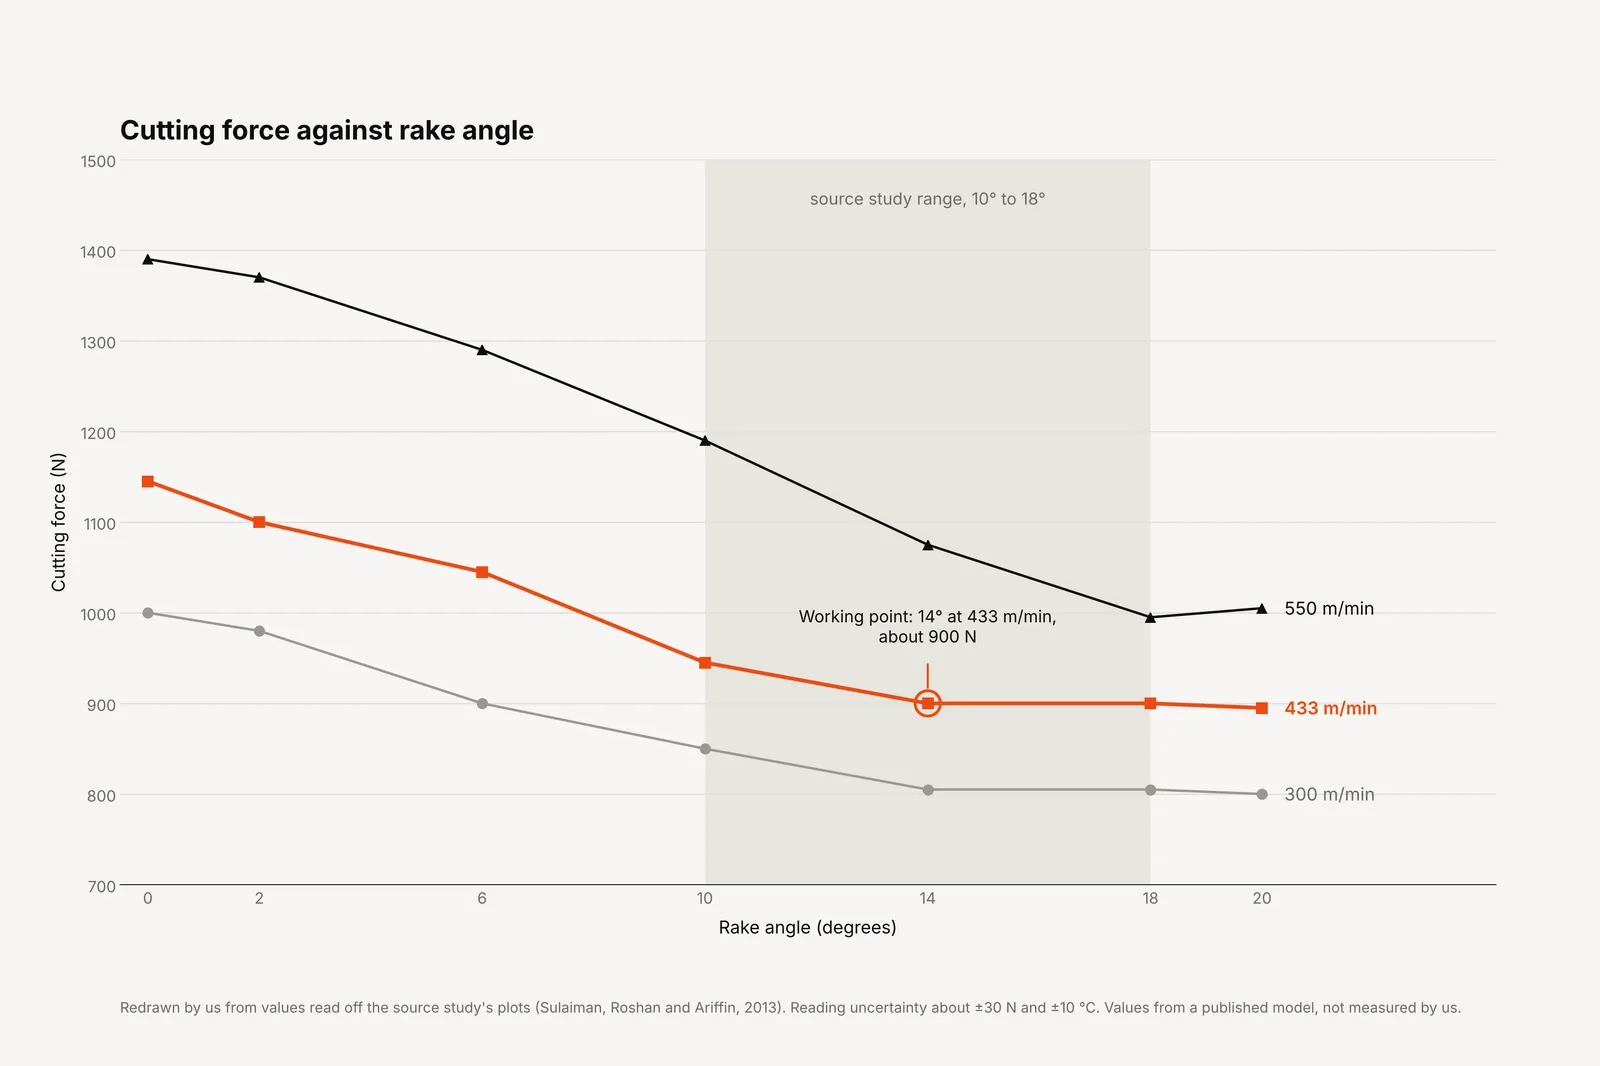
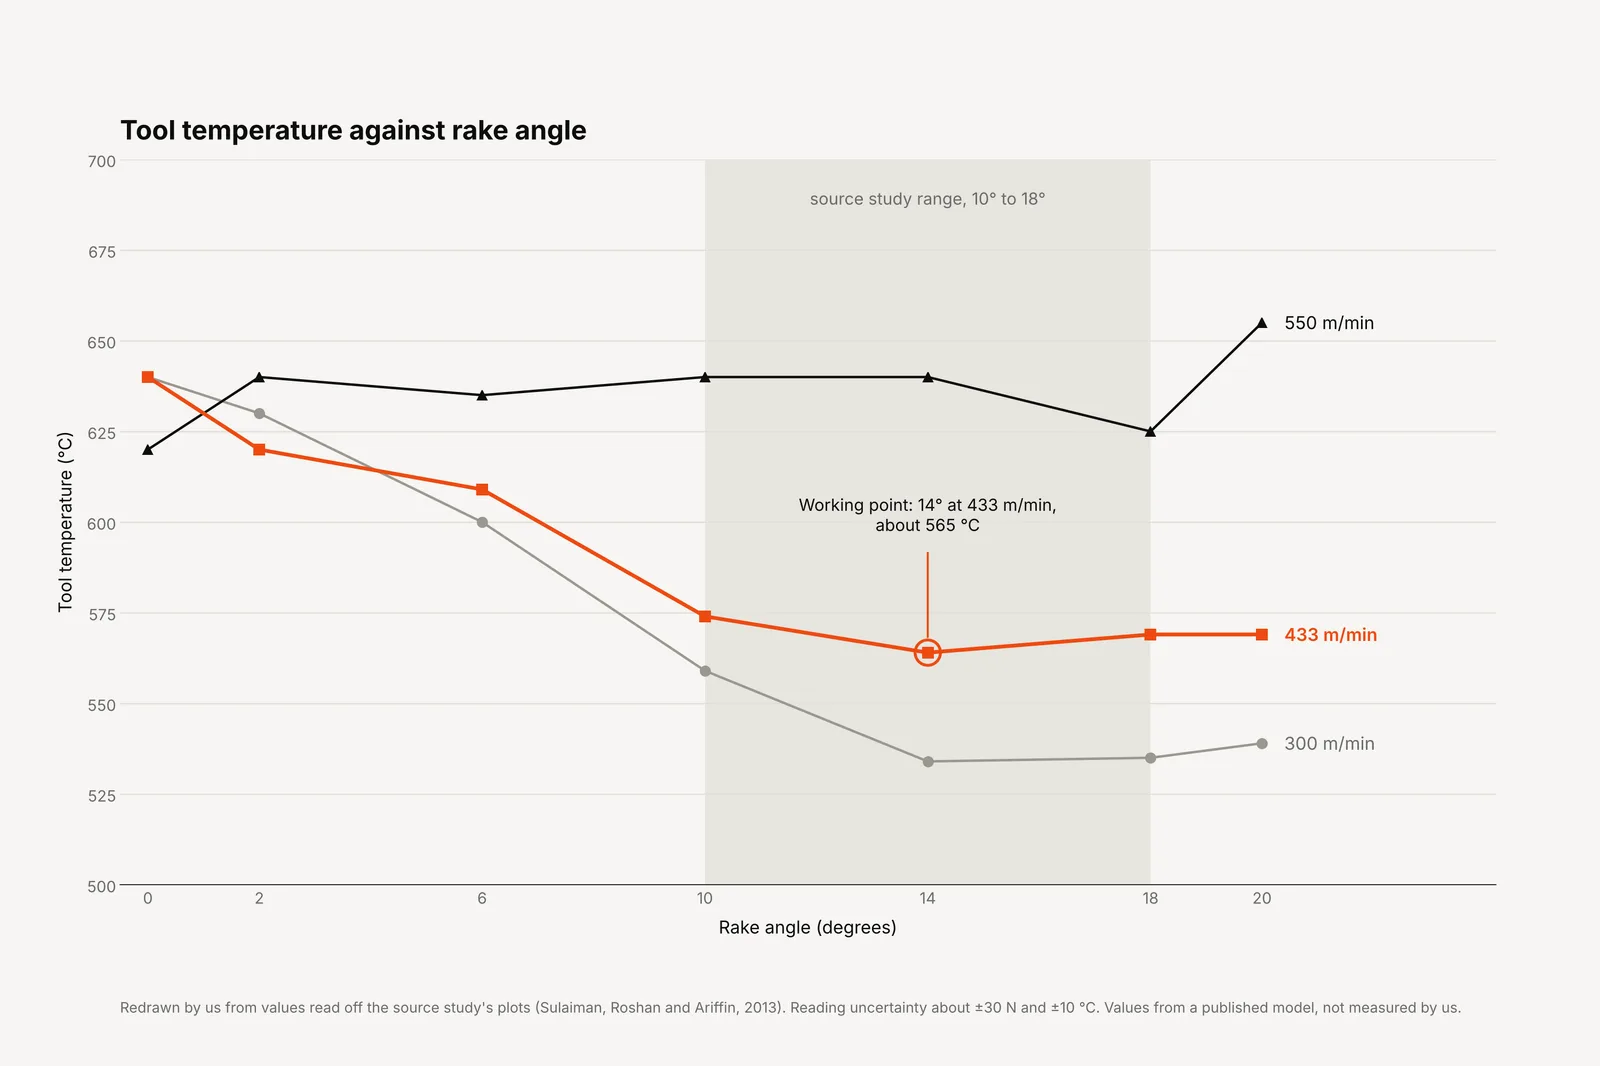
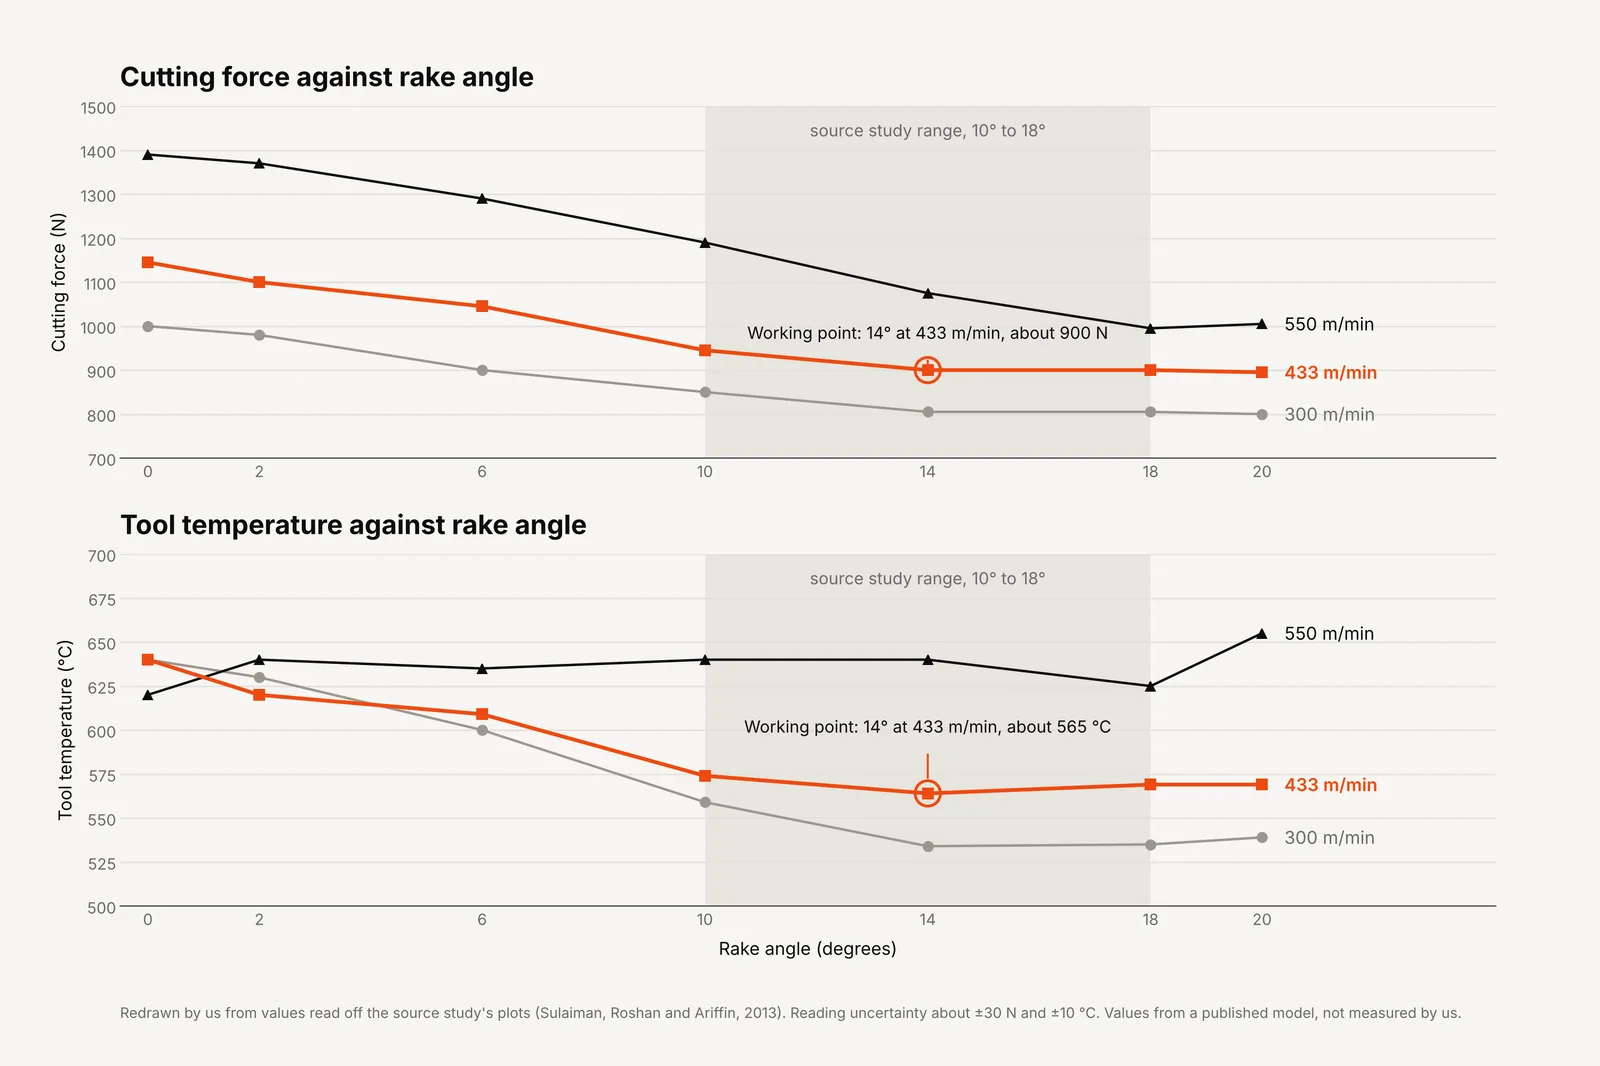
Force and tool temperature against rake angle at 300, 433 and 550 m/min. Values come from a published model (Sulaiman, Roshan and Ariffin, 2013), redrawn by me from the source plots, with a reading uncertainty of about 30 N and 10 degrees Celsius. I did not measure them. The source range is 10 to 18 degrees, and the working point of 14 degrees at 433 m/min sits near 900 N and 565 degrees Celsius.